Process Engineer Jobs

5,555 jobs found — updated daily

Senior Process Engineer
Cuisine Solutions•Sterling, VA

About The Position

The Senior Process Engineer provides strategic and hands-on leadership for engineering, maintenance, reliability, automation, utilities, facilities, and capital project activities in a sous vide food manufacturing environment. The role ensures plant equipment, infrastructure, and technical systems support safe, compliant, efficient, high-quality production of refrigerated and ready-to-eat food products. It partners with Operations, Quality Assurance, Food Safety, Sanitation, Supply Chain, Finance, and Executive Leadership to improve equipment reliability, production uptime, processes, regulatory compliance, and long-term manufacturing capability. The position is a key member of the site leadership team and typically reports to the President of Engineering and the Vice President of Engineering. It has no direct reports, though the role description includes leadership, coaching, and development of technical teams. Work takes place in office and food manufacturing plant environments, including refrigerated, wet, hot, and high-noise production areas. Availability outside normal business hours and travel of 40–60% as needed are required.

Requirements

  • Bachelor's degree in Engineering, Manufacturing Engineering, Mechanical Engineering, Electrical Engineering, Industrial Engineering, or a related technical field.
  • At least 15 years of progressive engineering, maintenance, reliability, or technical operations experience in food manufacturing, refrigerated foods, ready-to-eat foods, protein processing, sous vide, aseptic, pharmaceutical, or another highly regulated manufacturing environment.
  • At least 7 years of leadership experience managing engineering, maintenance, reliability, automation, or facilities teams in a 24/7 manufacturing operation.
  • Demonstrated experience leading capital projects, plant expansions, equipment installations, automation upgrades, and commissioning activities.
  • Strong knowledge of preventive and predictive maintenance, CMMS systems, maintenance planning, reliability-centered maintenance, root cause analysis, and spare parts management.
  • Working knowledge of food safety and regulatory programs, including HACCP, GMPs, sanitation design, allergen control, environmental monitoring, GFSI standards such as SQF or BRC, and OSHA requirements.
  • Experience with refrigeration, boilers, thermal processing, chilled water systems, vacuum packaging, cook/chill operations, PLCs, HMIs, SCADA, conveyors, utilities, and plant infrastructure.
  • Strong financial acumen, including budget preparation, capital justification, return-on-investment analysis, vendor management, and cost control.
  • Leadership, communication, problem-solving, project management, and cross-functional collaboration skills.
  • Ability to read and interpret PFD, P&ID, ISO, and DWG drawings.
  • Working knowledge of AutoCAD, Bluebeam, Procore, Microsoft Excel, Microsoft Project, and other software as required.
  • Ability to regularly walk production floors and access equipment areas, utilities, and mechanical spaces.
  • Availability outside normal business hours to support operations and critical events as needed.
  • Ability to travel 40–60% as needed.
  • Compliance with company safety, food safety, GMP, personal protective equipment, and sanitation requirements.

Nice To Haves

  • Advanced degree.
  • Strategic thinking and ability to translate business goals into practical engineering priorities.
  • Hands-on technical leadership and comfort engaging directly with equipment, technicians, operators, and supervisors.
  • Change leadership and ability to build structure, accountability, and consistency in a fast-paced production environment.
  • Ability to balance production needs, food safety requirements, capital constraints, and long-term reliability goals.
  • Data-driven decision-making focused on measurable improvements in safety, uptime, quality, yield, labor efficiency, utilities usage, and maintenance cost.
  • Experience with standardized subcontractor RFQs, technical OEM approval drawing reviews, OEM FAT and PAT, competitive bid review, and standardizing plant material selection and equipment installation methods.
  • Continuous improvement mindset and experience standardizing processes and developing technical talent.

Responsibilities

  • Develop and execute the plant engineering strategy to improve safety, quality, food safety, throughput, labor efficiency, equipment uptime, sanitation effectiveness, and cost performance.
  • Assist with capital planning and execution, including project scoping, budget management, vendor selection, contractor oversight, installation, commissioning, startup, and post-project performance validation.
  • Provide technical leadership for sous vide processing systems, cook tanks, chill systems, vacuum packaging equipment, boilers, refrigeration, compressed air, water and wastewater systems, conveyors, automation, controls, PLCs, HMIs, and facility infrastructure.
  • Partner with Quality Assurance and Food Safety to ensure engineering practices support HACCP, GMP, GFSI/SQF or BRC requirements, USDA/FDA expectations as applicable, allergen controls, sanitation design, hygienic zoning, environmental monitoring, and food defense programs.
  • Drive continuous improvement using root cause analysis, 5-Why, A3, Lean manufacturing, Six Sigma, standard work, and data-driven problem solving.
  • Ensure engineering and maintenance activities comply with OSHA, LOTO, electrical safety, applicable ammonia or refrigeration safety requirements, environmental regulations, company safety standards, and local building codes.
  • Lead engineering, maintenance, reliability, facilities, utilities, and automation functions for a high-volume sous vide food manufacturing plant.
  • Build, coach, and develop technical teams, including maintenance managers, engineers, supervisors, planners, technicians, controls specialists, and project resources.
  • Manage engineering and maintenance budgets, capital expenditures, contractor spend, utilities usage, MRO inventory, and cost-reduction initiatives.
  • Support new product introductions, line extensions, process validations, packaging changes, capacity expansions, and automation improvements.
  • Establish engineering standards, project management practices, sanitation-ready equipment design expectations, documentation controls, and technical training programs.
  • Serve as a key member of the plant leadership team, providing communication, risk assessments, project updates, and technical recommendations to senior leadership.
  • Conduct ROI capital analysis, standardized subcontractor RFQs, technical OEM approval drawing reviews, and OEM FAT and PAT activities.
  • Review and analyze competitive subcontractor bids.
  • Standardize plant material selection and methods for equipment installation.
  • Read and interpret PFD, P&ID, ISO, and DWG drawings.
  • Walk production floors, access equipment areas, inspect utilities and mechanical spaces, and respond to operational issues.
  • Support plant operations, critical downtime events, project installations, audits, inspections, and emergency response needs outside normal business hours as required.
  • Comply with company safety, food safety, GMP, personal protective equipment, and sanitation requirements.

Career Resources

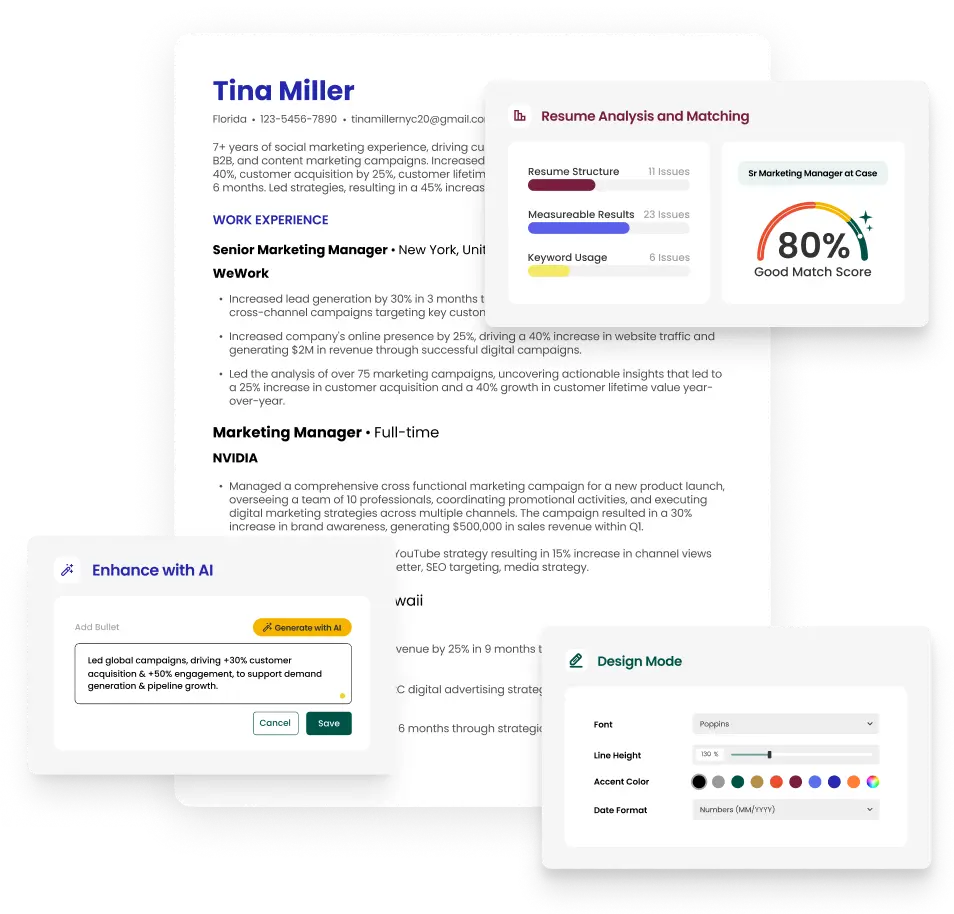
Build a Resume for Process Engineer

The resume builder that gets results.

  • Get clear feedback so you look as qualified as you are
  • Align your resume with the job to get further in the process, faster
  • Take the guesswork out of resume writing

Explore Related Job Searches

© 2026 Teal Labs, Inc
Privacy PolicyTerms of Service